CNC / TOOLING / RUNOUT
One Flute Is Doing All the Work. How Tool Runout Changes Chip Load
Mateusz Żuławski
CNC Programmer Setter Operator at Newby Foundries
≈ 4 min read
Same feed rate. Same spindle speed. Same programmed chip load. Different cutting conditions.
A four-flute cutter is designed to distribute the cutting load across four edges.
But what happens when the tool does not rotate concentrically?
Tool runout can change the effective radial position of each cutting edge. One flute may engage more aggressively, carrying a disproportionate share of the cutting load, while the others remove less material.
The result can be uneven flute wear, increased cutting forces, vibration, poorer surface finish and reduced tool life.
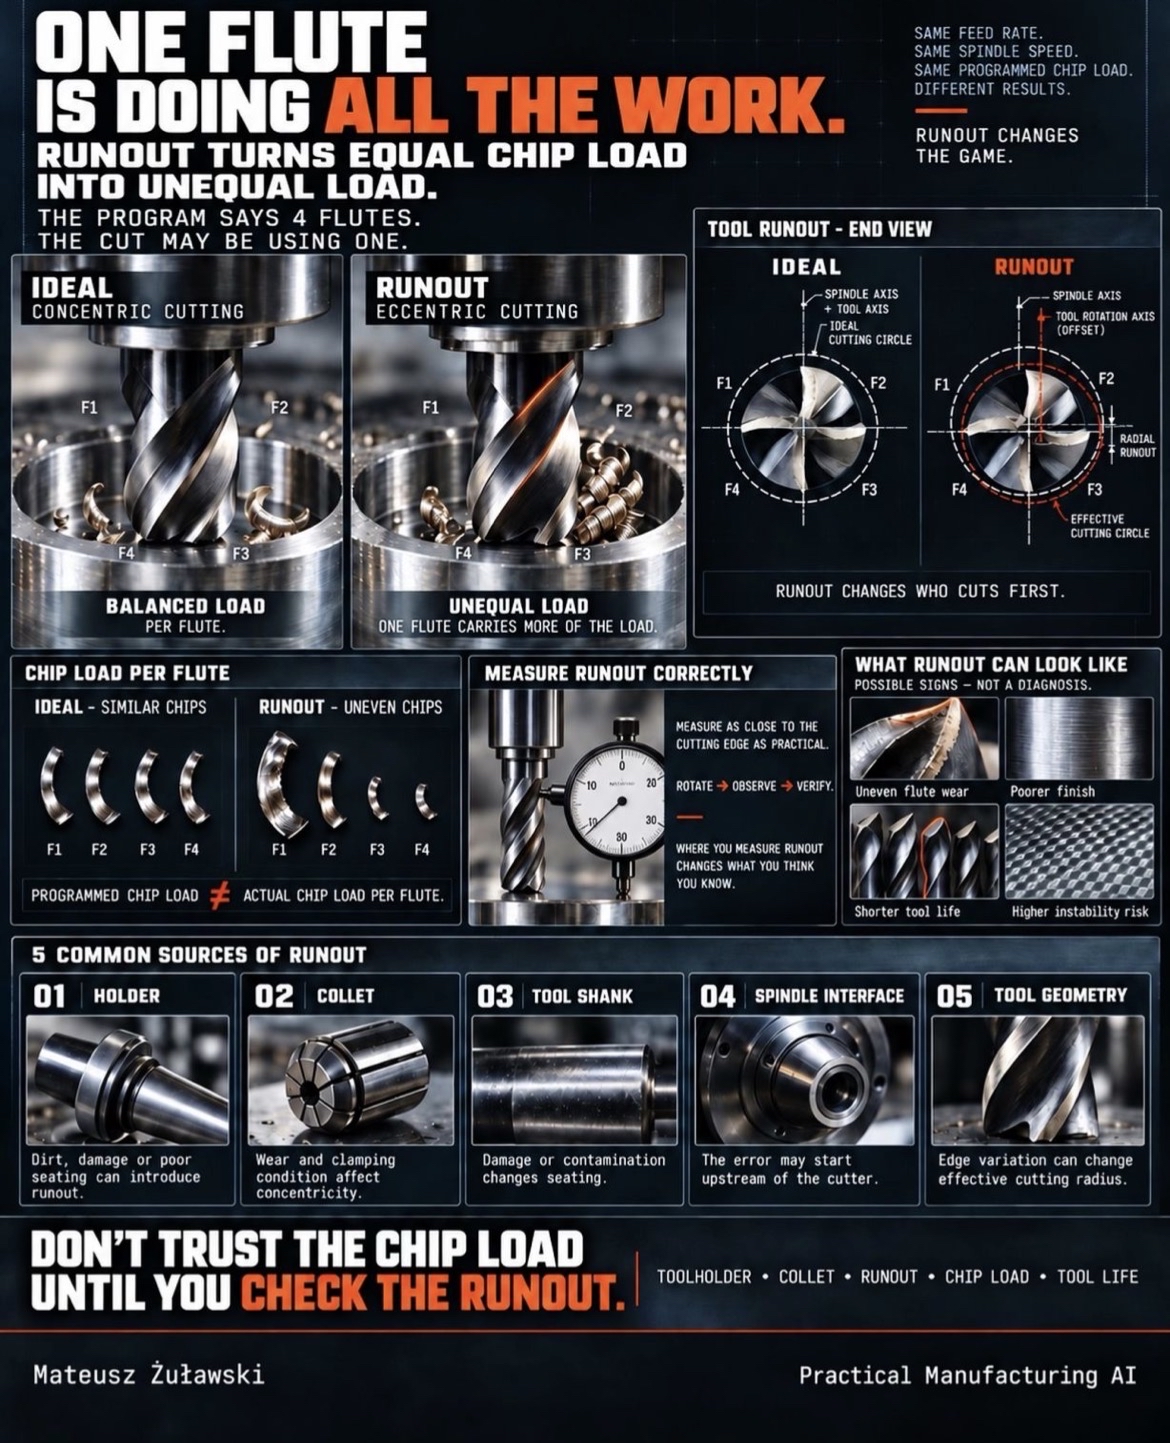
1. Ideal cutting vs cutting with runout
In an ideal setup, the tool rotates concentrically with the spindle axis. The cutting edges follow their intended paths, allowing the cutting load to be distributed more evenly.
With radial runout, the effective cutting radius varies between flutes.
The flute extending furthest from the rotational axis may remove a thicker chip and carry more of the load. Other flutes may contribute less than expected.
This is why the programmed feed per tooth does not necessarily describe the actual chip load experienced by every cutting edge.
Important: runout does not automatically mean that only one flute cuts. The actual load distribution depends on runout magnitude, tool geometry, engagement, material and cutting conditions.
2. What does runout actually change?
Runout affects the effective trajectory of the cutting edges.
When the radial position of each flute differs, the actual chip thickness and cutting force can become uneven.
Potential consequences include:
- Uneven flute wear.
- Increased local cutting forces.
- Vibration and process instability.
- Poorer surface finish.
- Reduced tool life.
The programmed parameters may remain exactly the same while the physical cutting conditions change.
3. Where can runout come from?
Do not assume the cutter itself is always responsible. The problem can originate anywhere in the toolholding assembly.
01 — Toolholder
Dirt, damage, poor seating or a damaged contact surface can introduce runout.
02 — Collet
Wear, contamination or incorrect clamping conditions can affect concentricity.
03 — Tool shank
Damage, contamination or geometric deviations can affect how the tool seats.
04 — Spindle interface
Contamination or damage at the spindle-to-holder interface can introduce errors upstream of the cutter.
05 — Tool geometry
Variations in flute geometry or effective cutting radius can produce uneven cutting conditions even when the holder assembly is correctly seated.
4. How to measure runout correctly
A dial indicator can help identify runout, but the measurement location matters.
A practical inspection sequence:
- 1. Clean the spindle taper, holder, collet and tool shank.
- 2. Check all contact surfaces for damage or contamination.
- 3. Assemble the tool correctly, following the manufacturer’s instructions.
- 4. Use a suitable dial indicator or runout measuring device.
- 5. Rotate the spindle manually, with the machine safely stopped and following the machine manufacturer’s procedure.
- 6. Measure at an appropriate point on the shank and, where the geometry allows, as close to the cutting edges as practical.
- 7. Compare readings and investigate whether reseating or indexing the tool changes the result.
A measurement at the shank does not always represent the actual runout at the cutting edges. Tool overhang and cutting geometry matter.
Do not place a measuring tip against a sharp cutting edge unless the measuring equipment is specifically designed for that method.
5. What can runout look like in production?
Possible signs include:
- One flute wearing noticeably faster than the others.
- Deteriorating surface finish.
- Shorter-than-expected tool life.
- Increased vibration or noise.
- Inconsistent results after a tool has been removed and reinstalled.
These are possible symptoms, not a diagnosis. Similar problems can also result from incorrect cutting parameters, tool deflection, spindle condition, insufficient workholding stiffness or material variation.
6. Do not compensate for a mechanical problem by changing parameters blindly
Reducing feed or spindle speed may reduce the load, but it does not remove the source of runout.
Check the complete assembly:
SPINDLE → TOOLHOLDER → COLLET → TOOL SHANK → CUTTER → CUTTING EDGES
Identify the cause before deciding what to change.
Also remember that tool runout and dynamic imbalance are not the same thing. They can occur together, but require different checks.
Final takeaway
The program may assume four flutes sharing the work. The real cutting process may tell a different story.
Tool runout can change the effective cutting radius, chip thickness and load carried by individual flutes.
That is why checking the complete toolholding assembly is an important part of controlling tool life, surface finish and process stability.
Don’t trust the programmed chip load alone. Check the runout first.
Question for CNC professionals:
Have you ever traced uneven cutter wear back to the holder, collet or spindle interface when the cutter itself appeared to be in good condition?